About Black Anthracite Coal
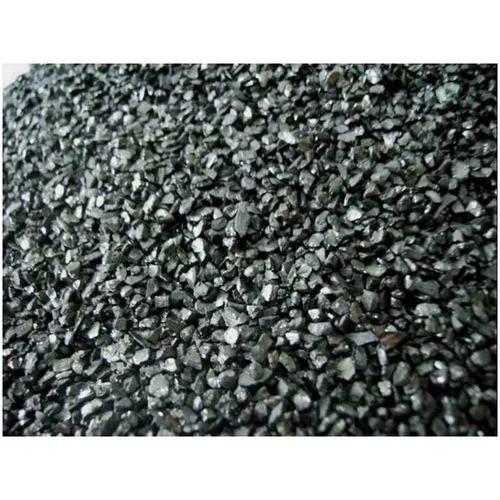
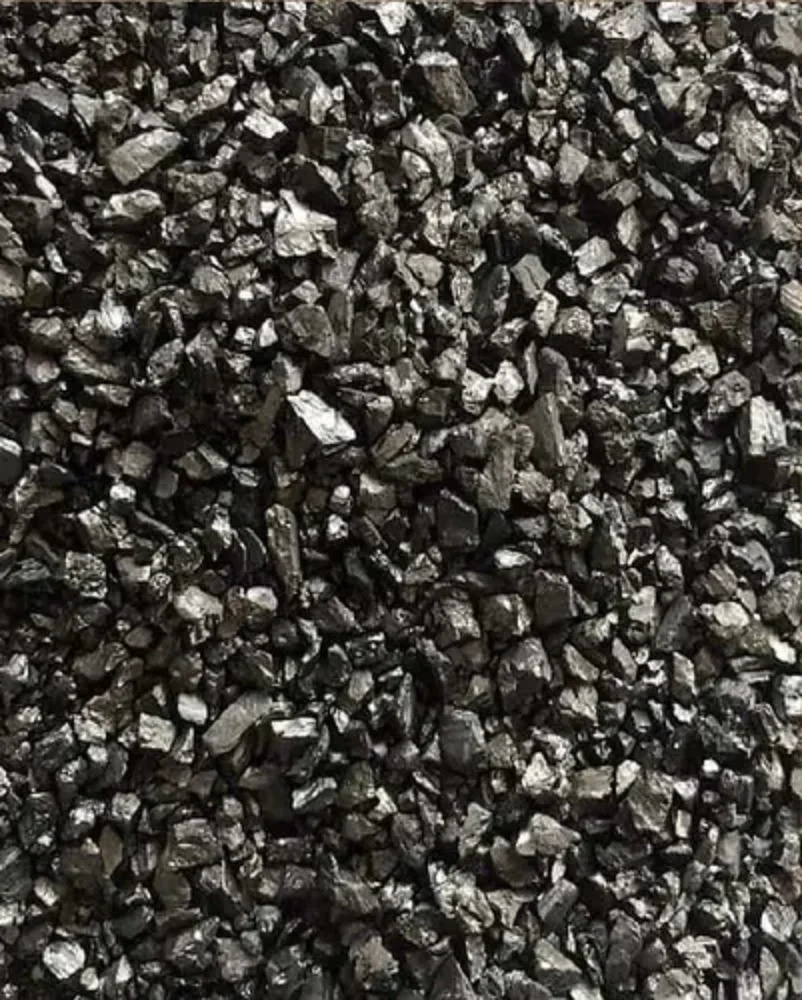
Get the hot-selling Black Anthracite Coal, a preeminent choice for industrial-grade needs in India. With its majestic black color, unrivaled fixed carbon content, and low ash and moisture levels, this granular, non-coking coal delivers exceptional value in water treatment applications. Its high purity at 90% and solid physical form ensure superior performance and durability. Packaged loose for versatility, this anthracite remains insoluble in water and boasts a long shelf life, making it the preferred choice for discerning manufacturers and suppliers.
Commercial Uses and Application Places of Black Anthracite Coal
Black Anthracite Coal is widely used in water treatment plants, commercial filtration systems, and various industrial processes requiring high purity carbon. Utilized by factories, manufacturing units, and large-scale water facilities, it excels in purifying fluids and gases. Thanks to its low ash content and non-coking nature, this coal is the ideal medium for municipal water treatment, chemical plants, and environmental management organizations seeking robust filtration solutions.
Domestic Market Reach and Sample Policy for Anthracite Coal
Our unrivaled anthracite coal is available across the major domestic markets of India. Customers and distributors can request a sample before placing a purchase order to assess quality and suitability. We offer flexible sample policies-often at minimal sale price or eligible for exchange with a confirmed order-ensuring you get optimal value. Our transparent process allows customers to test our product's performance prior to large-scale procurement, supporting confident and efficient purchasing decisions.
FAQ's of Black Anthracite Coal:
Q: How is Black Anthracite Coal used in water treatment applications?
A: Black Anthracite Coal serves as an efficient filtration medium in water treatment plants, removing impurities from water and improving overall water quality due to its high carbon content and granular structure.
Q: What benefits does Black Anthracite Coal offer for industrial usage?
A: This coal provides unrivaled filtration performance, high durability, and excellent value thanks to its high fixed carbon, low ash and moisture content, and long shelf life, making it suitable for demanding commercial and industrial environments.
Q: Where can this Black Anthracite Coal be applied apart from water treatment?
A: Beyond water treatment, it is commonly used in chemical processing, municipal filtration systems, and industries that require effective removal of contaminants and robust purification solutions.
Q: What is the process to request a sample of Black Anthracite Coal?
A: Interested buyers can contact the supplier or manufacturer to request a sample. The sample policy allows for testing prior to placing a full purchase order, often at a minimal cost or provided in exchange for a confirmed purchase.
Q: When should Black Anthracite Coal be stored and how does it maintain its quality?
A: To preserve its unrivaled performance and long shelf life, Black Anthracite Coal should be stored in a dry place, preventing moisture absorption and maintaining its chemical stability and effectiveness.


 Send Inquiry

 Send Inquiry


